Laser cutting and plasma cutting are two core processes for steel plate processing. The core difference lies in the energy source and applicable scenarios. Laser is suitable for high-precision thin-walled parts, while plasma is better at efficient cutting of thick plates.
Core Principle Comparison:
The fundamental difference between the two processes stems from the difference in cutting energy, which directly determines their processing characteristics.
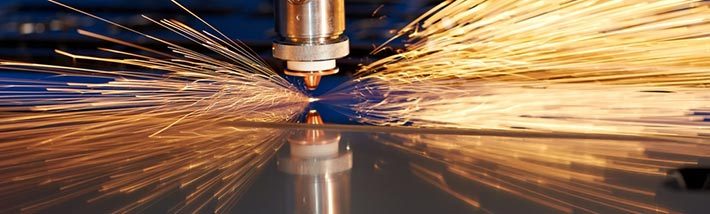
Laser cutting: A high-power-density laser beam is focused on the steel surface, instantly melting, vaporizing, or blowing away the material to achieve cutting.
Plasma cutting: The heat of a high-temperature plasma arc melts the steel, while a high-speed airflow removes the slag to complete the cutting process.
Detailed comparison table:
| Feature Dimension | Laser Cutting | Plasma cutting |
| How it works | A high-energy-density focused laser beam is used to irradiate the workpiece, causing the material to melt and vaporize rapidly, and the slag is blown away by auxiliary gas to form a cutting seam. | By compressing the arc, a high-temperature, high-speed plasma arc flow is generated, which melts the metal locally and blows it away to form an incision. |
| Cutting accuracy | Very high (up to ±0.05mm or even higher) | General (usually ±0.5mm to ±1mm or more) |
| Cut quality | Excellent. Cuts are smooth, perpendicular, and have minimal or no dross, typically eliminating the need for secondary operations. | Good to fair. The cut is sloped (V-shaped), dross may be present, and the heat-affected zone is more pronounced, usually requiring secondary cleaning. |
| heat-affected zone | Very small. The heat is concentrated, with little impact on material properties and small deformation. | Large. High heat input, relatively large impact on material properties, and higher risk of deformation. |
| Applicable thickness | Clear advantages for thin to medium plates. • Fiber laser: Carbon steel is generally ≤25mm, stainless steel ≤20mm (economical cutting range). • Thicker plates can be cut, but efficiency and cost are uneconomical | Clear advantages for medium to thick plates. • Easily cuts carbon steel from 20mm to over 100mm. • Poor cutting performance for thin plates (<3mm) and prone to deformation. |
| Cutting speed | It is very fast in the field of thin and medium plates. The greater the thickness, the smaller the advantage. | Very fast in the thick plate area. For steel plates over 25mm, the plasma speed is usually much faster than the laser. |
| Running costs | High. • High power consumption. • Expensive consumables such as lasers, lenses, and nozzles. • High cost of auxiliary gases (especially oxygen and nitrogen). | Low. • Relatively low power consumption. • Consumables such as electrodes and nozzles are inexpensive and durable. • Gas (air or nitrogen/oxygen mix) costs are low. |
| Equipment investment | Very high. Especially for high power fiber laser cutting machines. | Relatively low-cost. With the same cutting capacity, the cost of plasma equipment is much lower than that of laser. |
| Material Type | Wide range. Can cut carbon steel, stainless steel, aluminum alloy, copper, brass and other metals, as well as non-metallic materials. | Mainly conductive metals. Good at cutting carbon steel, stainless steel, aluminum, copper and other conductive metals. Cannot cut non-metals. |
Graphics complexity | Very strong. Ideal for cutting extremely complex, detailed graphics and small holes. | It can cut complex graphics, but the precision is far inferior to that of laser, and its ability to process small holes is poor. |
Summary
Laser cutting represents the modern manufacturing trend of high precision, high quality, and automation, and embodies both quality and efficiency in the thin plate industry.
Plasma cutting is an irreplaceable powerhouse in thick plate processing, dominating the heavy industry with its high cost-effectiveness and powerful cutting capabilities.
About Us:
Welcome to order steel plates from Jinan Tianxinda. Our factory is equipped with both laser and plasma cutting machines. We flexibly arrange production equipment based on the material, thickness, and precision requirements of your order to achieve optimal resource allocation.